Production technologies
PVC profile extrusion, rigid and flexible
We extrude plastic profiles and gaskets with a constant cross-section – from rigid and soft PVC, TPE, ABS and PP, including co-extrusion. A technology of RefPlast, a brand of the AiFO Group.
Why extrusion
One profile instead of several parts
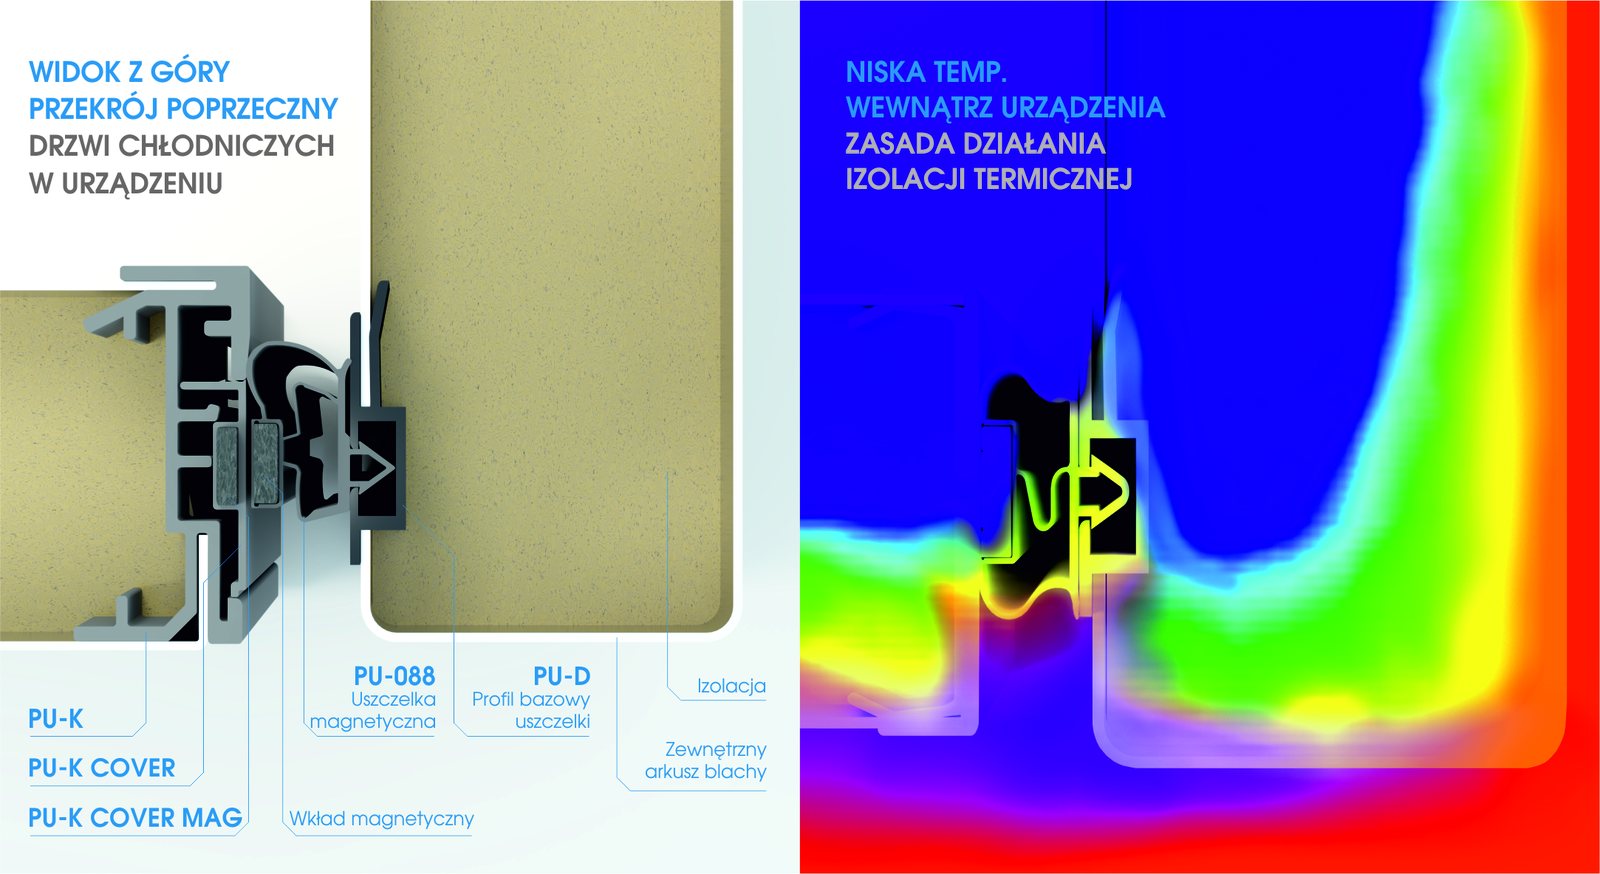
Extrusion delivers any cross-section you need along the entire length of the part – from a simple strip to a profile with air chambers that eliminate thermal bridges.
In co-extrusion we combine two plastics in a single cycle, for example rigid PVC with soft TPE, so the gasket is formed together with the profile and needs no separate assembly.
What we make
Extruded profiles for refrigeration
Thermal-bridge profiles
Cross-sections with air chambers that limit heat losses in the most critical spots of refrigeration equipment.
Door profiles
A wide range of shapes for refrigeration doors, compatible with many glass pane and door system models.
Glass cover profiles
Profiles for in-store equipment that give easy access to the product and a clear presentation.
LED profiles
Profiles for LED strips in various shapes and sizes, easy to match to the fittings in use.
What you gain
Why extrude with us
Repeatability and precision
Lines with automatic dimensional control keep the cross-section within tolerance across the whole run.
A continuous process
Extrusion runs without interruption, so short lead times are possible even at high volumes.
Co-extrusion
We combine two polymers in one cycle – rigid PVC with soft TPE, or layers with different properties.
Any length
We cut the profile to the length given by the customer, in very long or very short versions alike.
Through-colouring
Pigments are added during plasticising, so the colour is permanent and does not rub off the surface.
Ready for further processing
We prepare the profiles for the next steps – cutting, batch marking or welding.
Technical parameters
Materials and line capabilities
- Materials
- Rigid and soft PVC, TPE, ABS, PP
- Technology
- Single- and multi-layer extrusion (co-extrusion)
- Cross-sections
- Simple and multi-chamber, to the customer's drawing
- Colour
- Through-colouring with pigments
- Finishing
- Cutting to length, printing, preparation for welding
- Batches
- From short runs to high-volume production
Production process
From the cross-section design to a finished profile
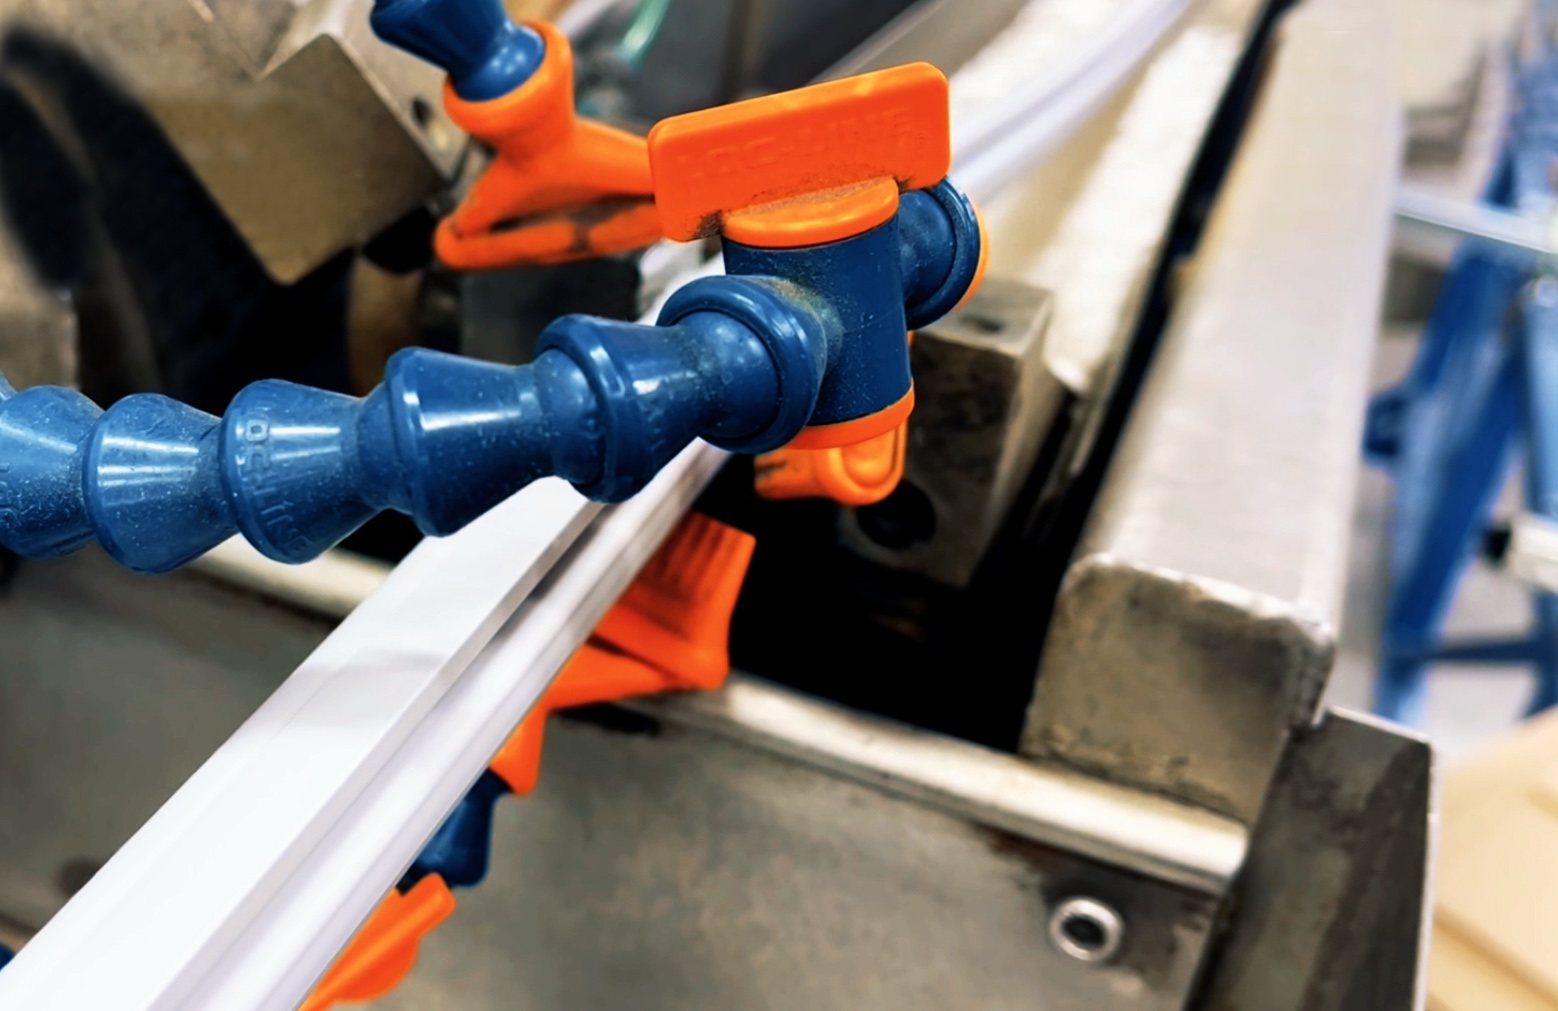
Extrusion is a continuous process – we plasticise the granulate, force it through the forming die, cool it and cut it to length.
-
Cross-section design
Our engineers prepare drawings and models of the profile, including complex multi-chamber cross-sections.
-
Plasticising the granulate
The granulate is heated to the temperature at which the plastic forms a homogeneous, mouldable mass.
-
Adjusting the composition
Additives that influence the colour and properties of the finished profile are mixed into the plasticised material.
-
Extrusion
The molten plastic is forced continuously through the forming die, which gives it its cross-section.
-
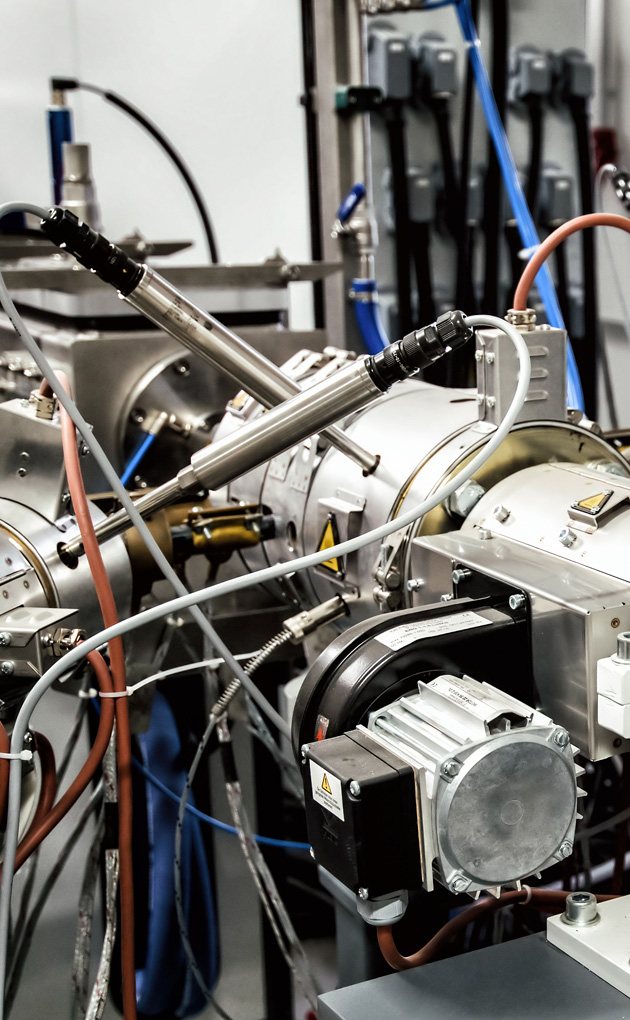
Cooling
The profile is cooled with nozzles to fix its shape and achieve stable dimensions.
-
Finished product
The profile is cut to length, marked with the batch number and prepared for further processes.
Applications
Where our profiles work
- Refrigerated furniture and shelving
- Refrigerated doors and display cases
- Cold and freezer rooms
- Glass covers of in-store equipment
- LED display lighting
- Catering furniture
Production technologies
See how production works
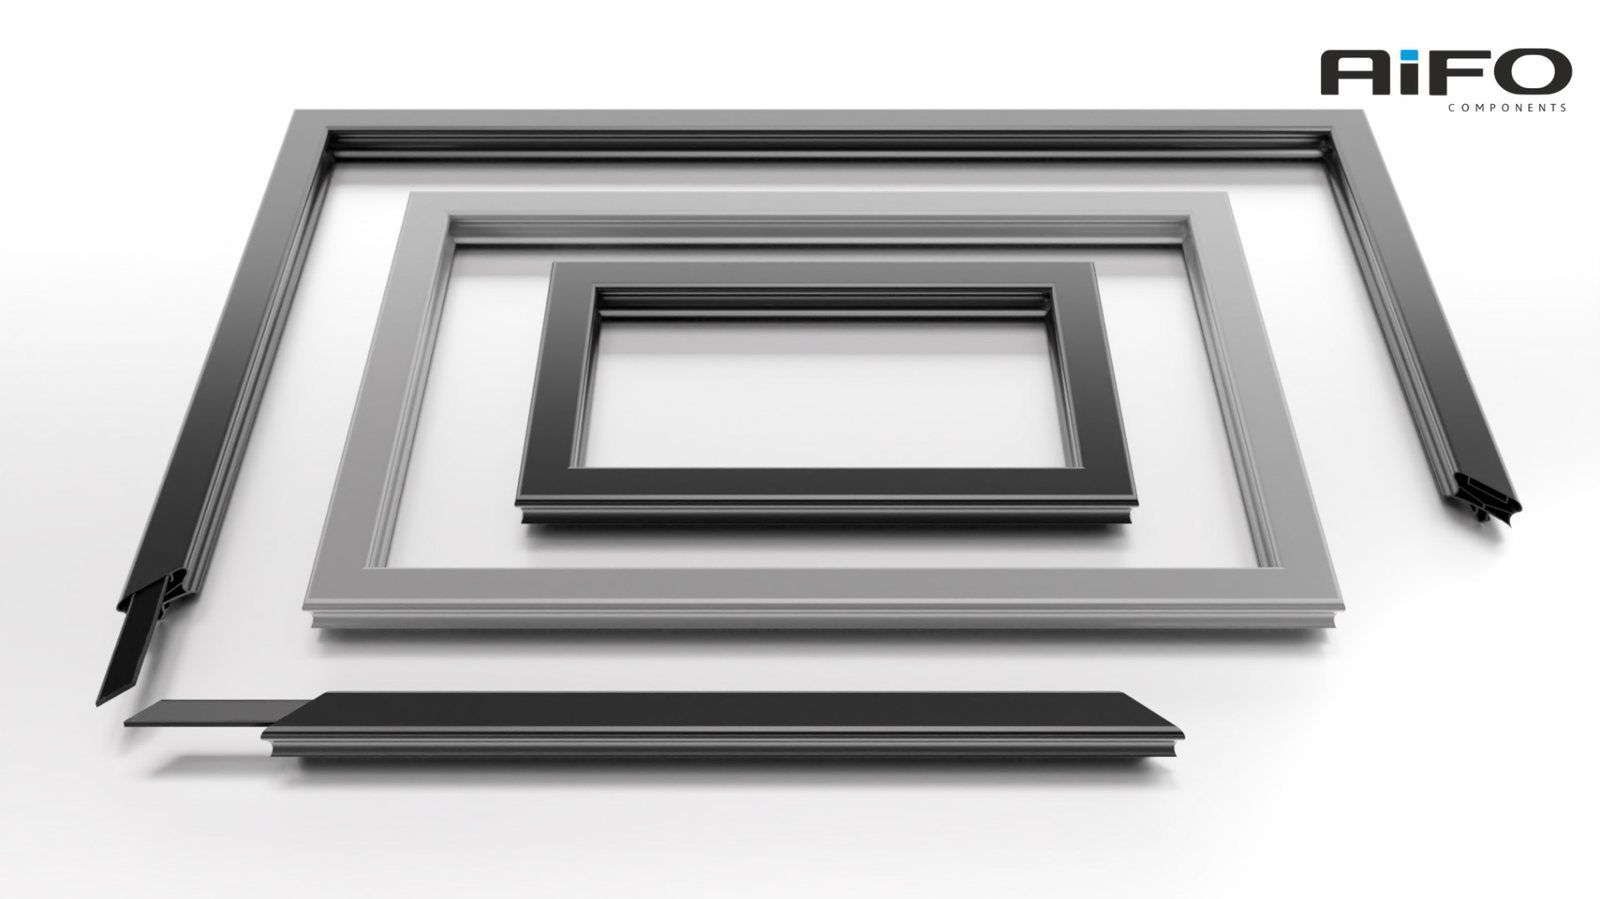
Welding of magnetic gaskets for refrigeration
Gaskets and magnetic inserts
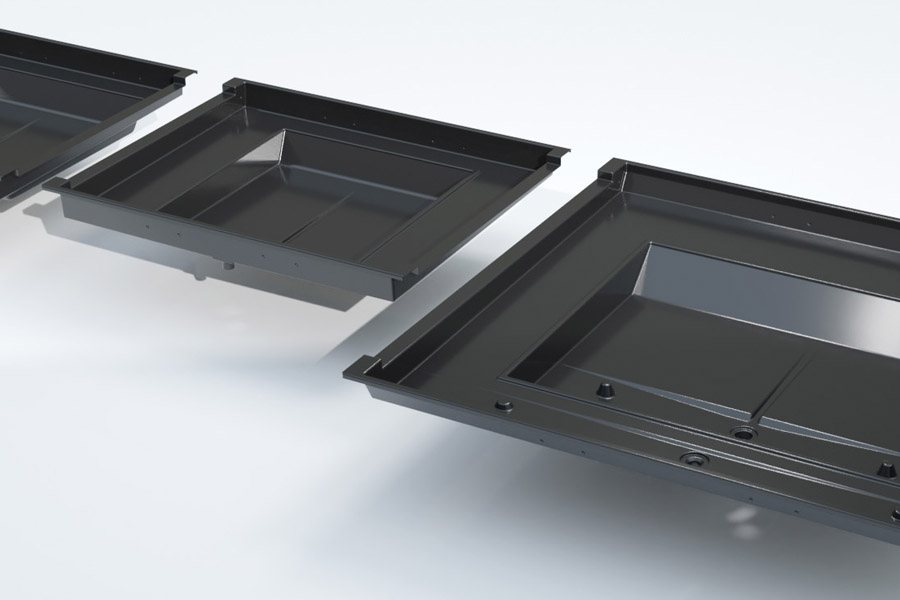
Thermoforming
Vacuum-formed parts
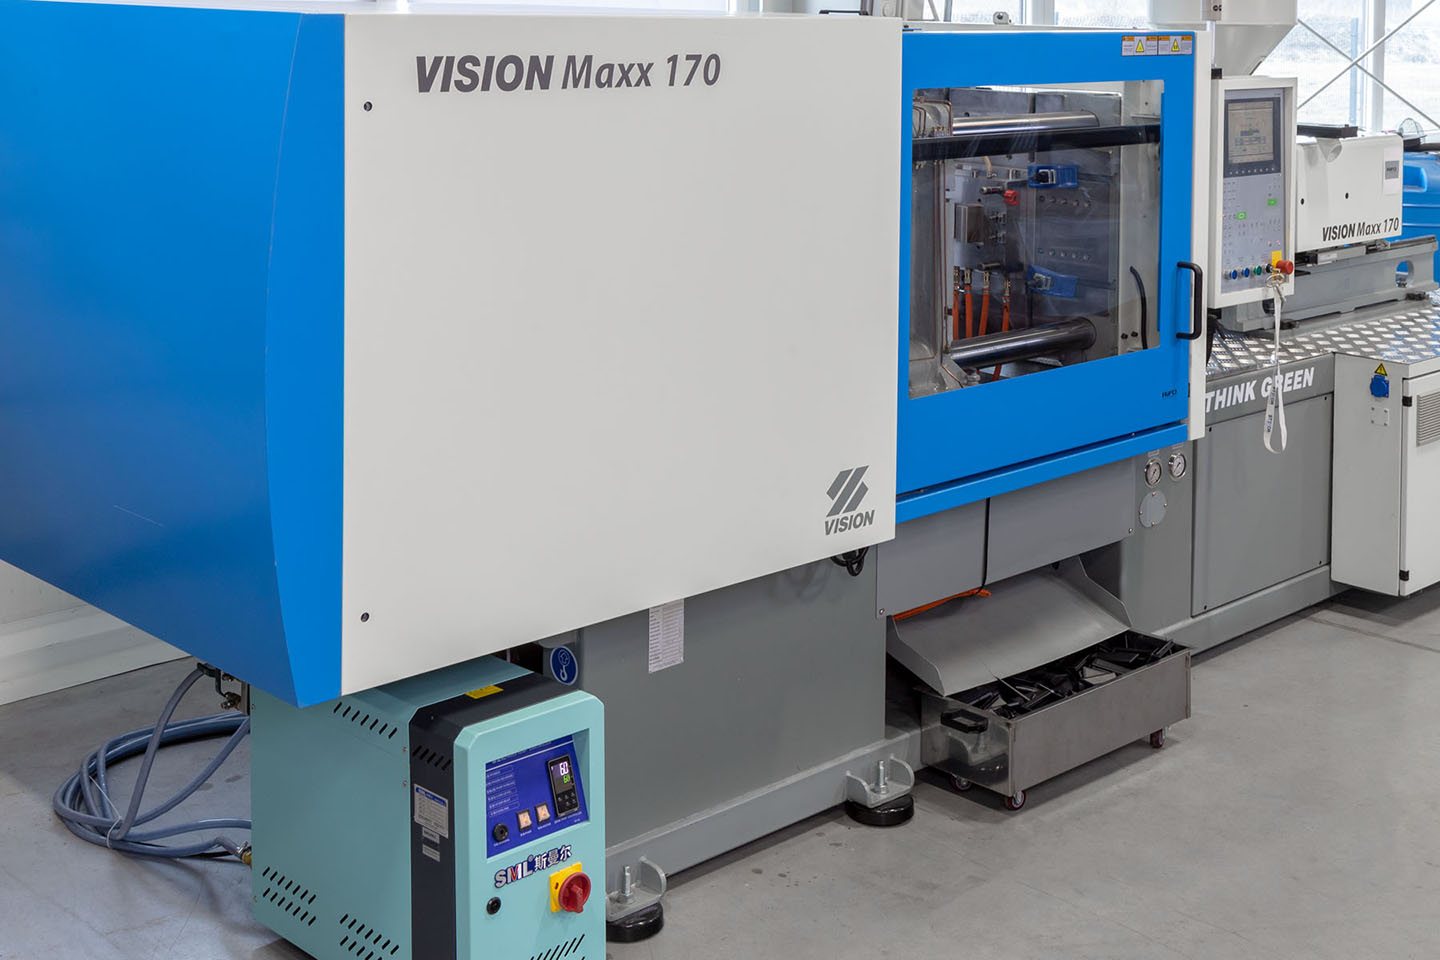
Plastics injection moulding
Moulded parts for refrigeration and HoReCa
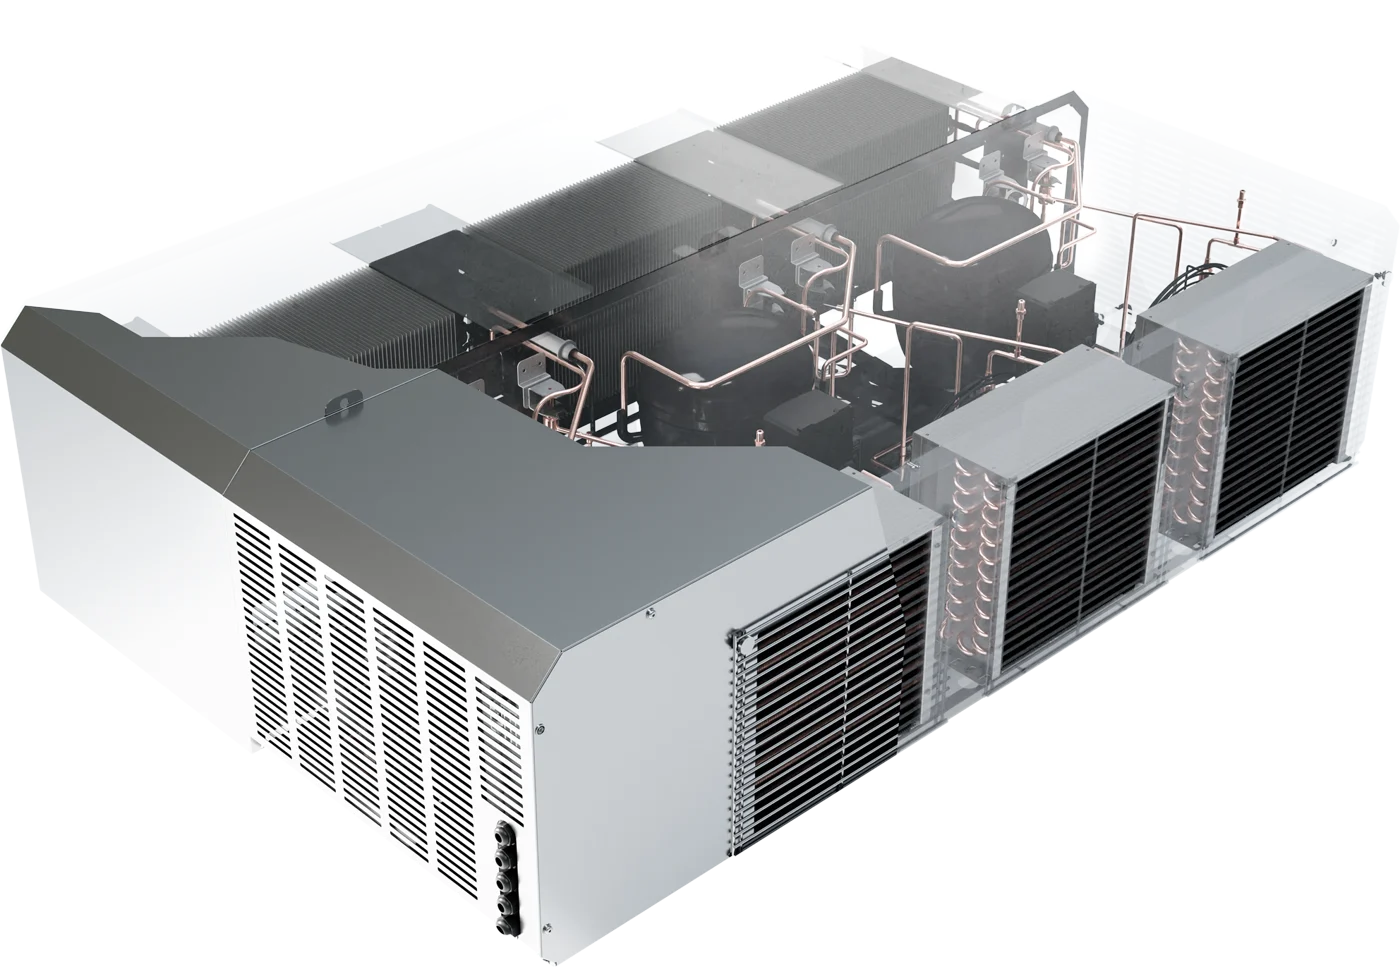
Monoblock chillers
Monoblocks and condensing units
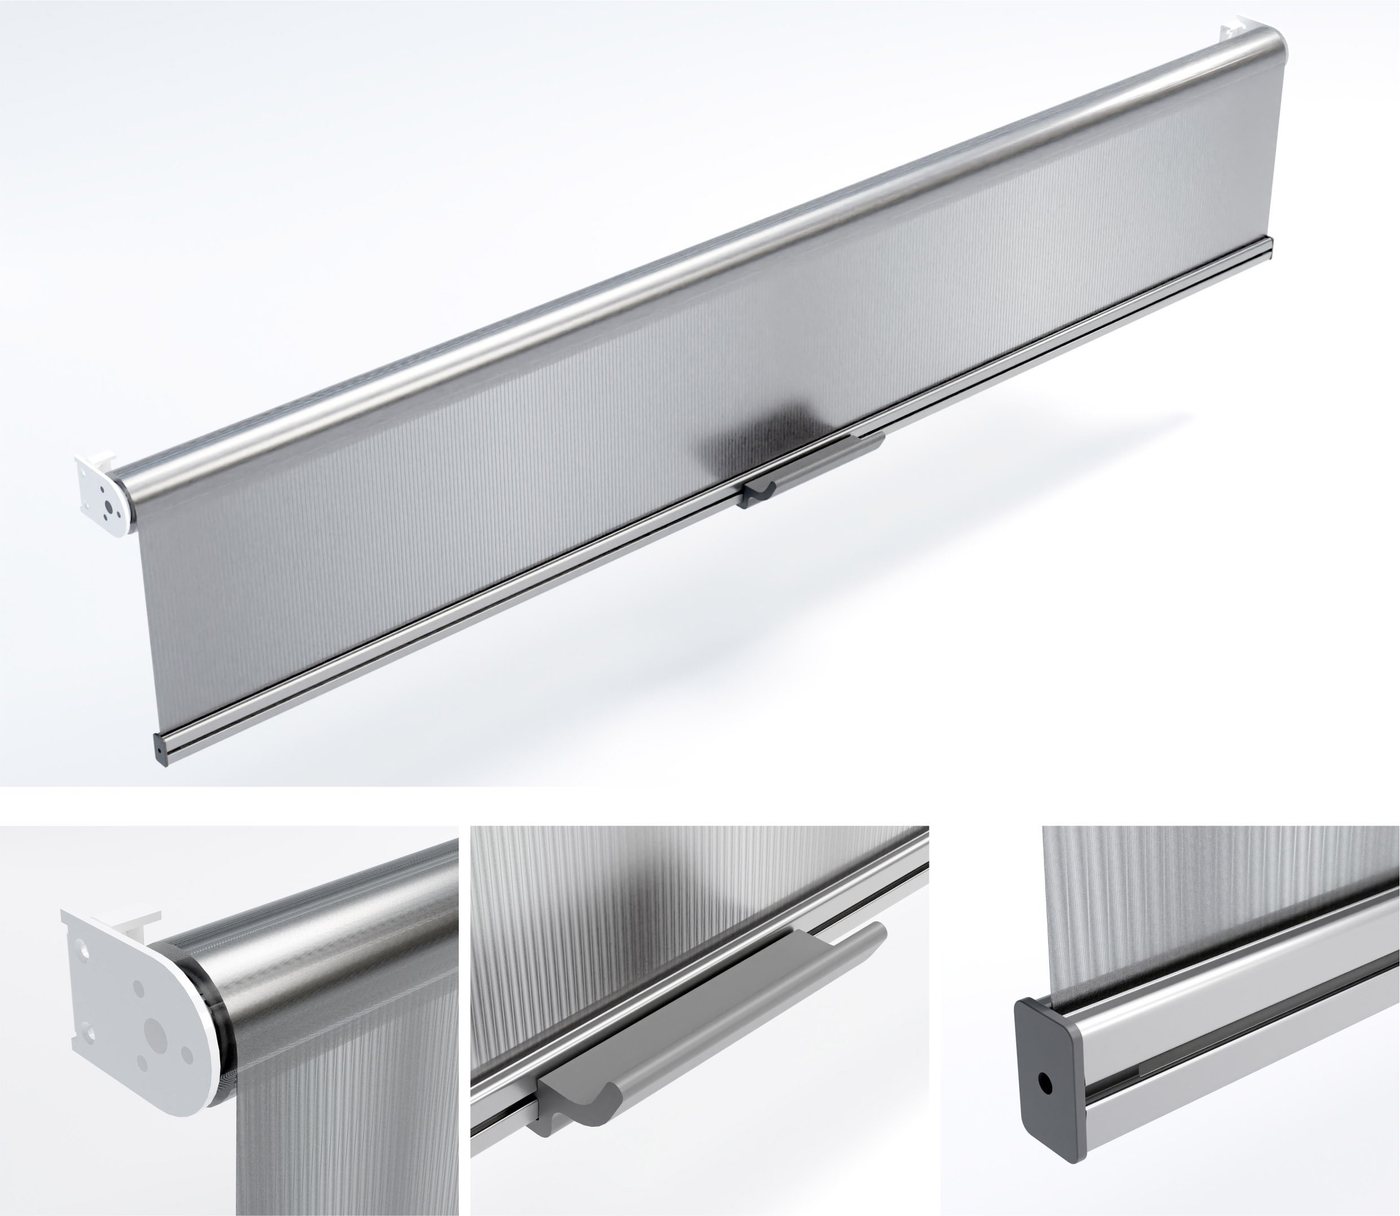
Roller blinds for refrigerated shelving
Blinds matched to the type of case
Thermal break profiles
Two profile families and custom sections
PU insulation of refrigeration furniture parts
Components with a polyurethane core
A profile designed around your appliance, not the other way round.
- PVC + TPE co-extrusion – a gasket integrated with the profile.
- Profiles with air chambers that eliminate thermal bridges.
- Through-colouring and cutting to any length.
FAQ
Frequently asked questions about plastics extrusion
Did not find your answer? Write to us – we will review the cross-section and select the material.
Ask a questionWhat is plastics extrusion?
It is a continuous forming process in which plasticised material is forced through a die that gives it a constant cross-section. This is how rigid PVC profiles, soft PVC gaskets and parts combining both materials are made.
What is co-extrusion?
Co-extrusion combines two or more plastics in a single cycle. Most often we join rigid PVC with soft TPE, so the gasket is formed together with the profile and needs no separate assembly.
Which materials do you extrude?
We work with rigid and soft PVC, TPE, ABS and PP. The material is matched to the operating temperature, the required stiffness and any food-contact requirement.
Will you make a profile to my drawing?
Yes. We extrude profiles from the customer's drawing, and where there is no drawing our engineers design the cross-section from scratch, based on a sample or a description of the application.
Can the profile be coloured?
Yes. Pigments are added while the plastic is being plasticised, so the colour runs through the whole cross-section and does not rub off the surface.
How long can the extruded profiles be?
The process is continuous, so in practice length is limited by transport and packaging. We cut the profile to the length stated in the order.
Discuss your project
We will design and extrude your profile
Send us a cross-section drawing or a sample – we will select the plastic and quote both the tooling and the production run.
Get in touch
We usually reply within 24 working hours.